Category
RX12 PET Bottle Blow Molding Machine
"Product advantage"
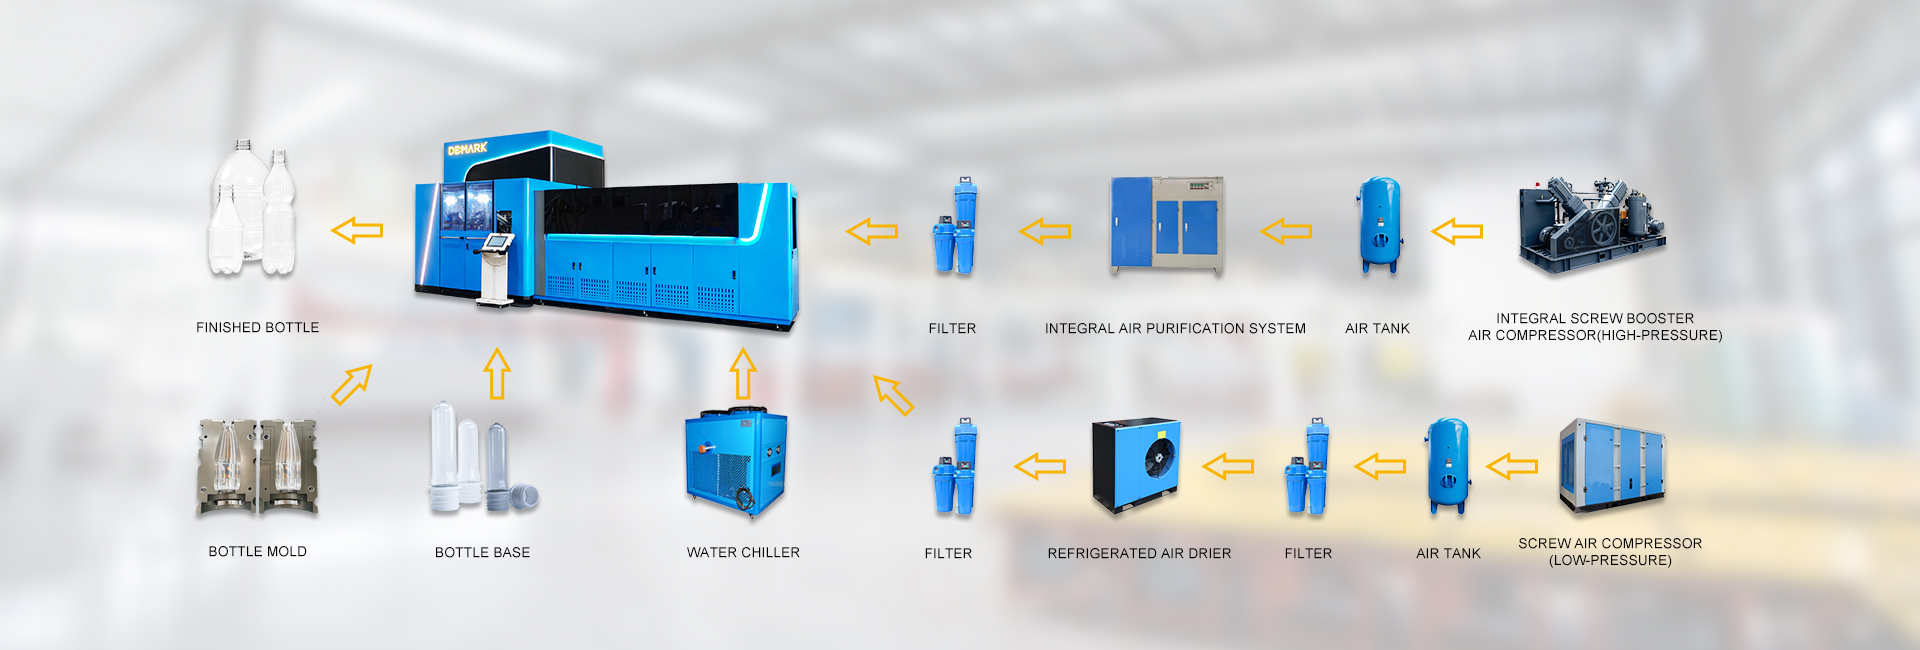
Discover the pinnacle of efficiency with our RX12 in the"Small Mould Base"category—a pet stretch blow molding machine designed to elevate your production capabilities. Engineered with precision, the RX12 boasts impressive specifications: 12 cavities ensuring seamless operation, a capacity of 28,800 bottles per hour (based on 500ml water bottles), and a volume range spanning from 200ml to 2500ml.
The RX12 Small mould base machine is tailor-made for diverse applications across multiple sectors. Whether you're bottling water, carbonated drinks, juices, dairy beverages, edible oils, or non-food items like cosmetics and detergents, the RX12 stands ready to optimize your manufacturing process. As a kind of high-speed blow molding machine, its robust build ensures consistent performance and reliability.
Elevate your operational capabilities with the RX12 pet stretch blow moulding machine, a cost-effective solution ideal for enhancing productivity and expanding product offerings. Crafted to meet the dynamic demands of markets, particularly in India, this automatic blow molding machine epitomizes innovation combined with industry-leading efficiency.
"Detailed information"
| Series | Type | Cavities | Capacity(based on 500ml water bottle) | Minimum volume(ml) | Maximum volume(ml) | Application |
| Small Mould Base | RX10 | 10 | 24000 | 200 | 750 | bottles of water, carbonated drinks, juice, dairy beverage, edible oil, cosmetics, detergent, daily products |
| RX12 | 12 | 28800 | 200 | 750 | ||
| RX14 | 14 | 33600 | 200 | 750 | ||
| RX16 | 16 | 38400 | 200 | 750 | ||
| RX18 | 18 | 43200 | 200 | 750 | ||
| RX20 | 20 | 48000 | 200 | 750 | ||
| RX22 | 22 | 49500 | 200 | 750 | ||
| RX24 | 24 | 54000 | 200 | 750 |
"Revolutionize Your Production Line: with the RX12 PET Bottle Blow Molding Machine"
The blow molding process of the bottle blowing machine is a bi-directional stretching process, in which the PET chains are stretched, oriented, and placed in both directions, thereby increasing the mechanical properties of the bottle wall, improving the tensile, tensile, and impact strength, and having excellent airtightness. Although stretching can help improve strength, it should not be excessively stretched. It is important to control the stretching inflation ratio: do not exceed 3.5-4.2 in the radial direction and 2.8-3.1 in the axial direction. The wall thickness of the preform should not exceed 4.5mm.
Blow molding is carried out between the glass transition temperature and the crystallization temperature, usually controlled between 90 and 120 degrees. In this range, PET exhibits a high elasticity state, and after rapid blow molding and cooling shaping, it becomes a transparent bottle. In the one-step process, this temperature is determined by the length of cooling time during the injection molding process (such as the Aoki blow molding machine), so it is necessary to connect the injection and blowing stations well.
In the blow molding process, there are three actions: stretching, first blowing, and second blowing. The duration of these three actions is short, but they must be well coordinated, especially the first two steps determine the overall dispersion of the material and the quality of the blown bottle. Therefore, it is necessary to regulate the starting and ending opportunities of stretching, stretching speed, pre blowing start and end opportunities, pre blowing pressure, pre blowing flow rate, etc. It is best to control the overall temperature distribution of the preform and the temperature gradient of the inner and outer walls of the preform.
- RX20 moulding blow machineThe RX20 molding blow machine is an efficient and stable production equipment that uses advanced technology and high-quality materials. It enables automated operation and precise control of volume and shape, making it widely used in the packaging manufacturing industry for food, medicine, cosmetics, and more. With its accurate mold design and high-speed production capabilities, it can greatly improve the production efficiency and competitiveness of enterprises, making it a significant choice in modern manufacturing.RX20Send Inquiry
- RX18 Rotary Blow Molding MachineExplore enhanced manufacturing capabilities with the RX18, a pinnacle of innovation in our "Small Mould Base" category. Featuring 18 cavities, this advanced machine achieves production speeds of up to 43,200 PET bottles per hour, based on 500ml water bottles. From 200 ml to 2500 ml, the RX18 accommodates a versatile range of bottle sizes, ensuring seamless adaptation to diverse packaging needs.RX18Send Inquiry
- RX16 PET Bottle Blow MolderEnhance your manufacturing efficiency with the RX16, an innovative addition to our "Small Mould Base" category. This state-of-the-art machine boasts 16 cavities, enabling production speeds of up to 38,400 PET bottles per hour, based on 500ml water bottles. Whether you need bottles ranging from 200 ml to 2500 ml, the RX16 adapts flawlessly to various sizes, ensuring versatility across different applications.RX16Send Inquiry
- RX10 PET Blowing MachineIntroducing the RX10, a high-capacity, fully automatic blow molding machine from our "Small Mould Base" series. With 10 cavities, it produces up to 24,000 bottles per hour, handling sizes from 250 ml to 2500 ml. Ideal for a variety of products including beverages and daily essentials, the RX10 boosts productivity and flexibility in production lines.RX10Send Inquiry
Send Message